How PCBA is actually tested: AOI, X-ray, ICT and functional test
"We test every board" is not a meaningful statement on its own. There are at least six different inspections a contract manufacturer can run, they catch different things, and none of them catches everything. Here is what each one actually does — and how to decide which ones your product needs.
- Before placementSPI
- After reflowAOI
- Hidden jointsX-ray
- Does it workElectrical test
The six inspections, and what each one is blind to
Read the third column before deciding how much inspection to buy — that is where the defect that reaches your customer comes from.
| Method | What it catches | What it cannot see |
|---|---|---|
| 3D SPI solder paste inspection | Paste volume, height and area after printing, before anything is placed. Catches a blocked stencil aperture or an underfilled pad. | Anything that goes wrong after printing. It says nothing about whether the part lands in the right place. |
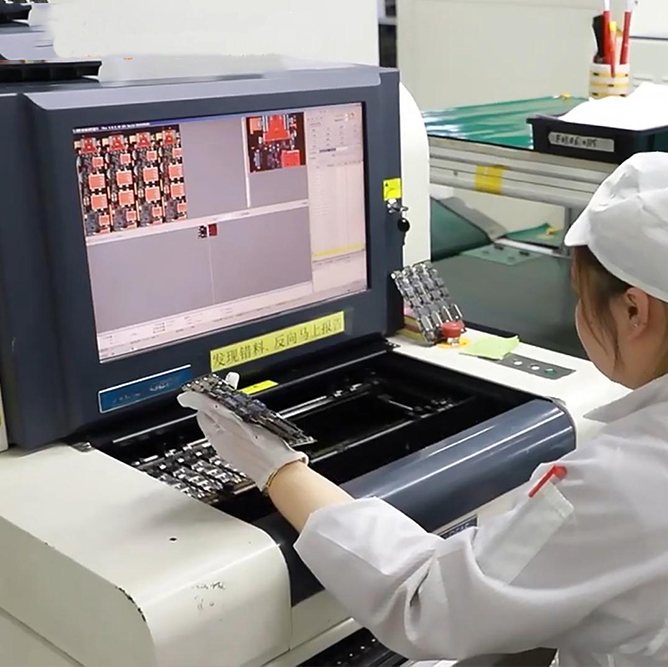
| AOI (pre-reflow) | Missing parts, wrong parts, reversed polarity, gross misalignment — before the joint is formed, so the fix is cheap. | Anything that has already been placed and shifted later. Nothing about the joint itself. |
| AOI (post-reflow) | Solder bridges, insufficient solder, missing parts, tombstoning, wrong orientation, damaged bodies. | Any joint under a package — BGA, QFN, LGA, chip-scale. Also grades by appearance, so it cannot tell a good joint from one that will fatigue. |
| 3D X-ray | BGA ball voids, opens and bridging under arrays, QFN thermal pad coverage, through-hole barrel fill, head-in-pillow. | Whether a part is electrically correct. A board with perfect joints can still be functionally wrong. |
| ICT / flying probe | Individual component presence and value, opens and shorts between nets, orientation of diodes and polarised parts. | Anything without a test point, and anything that only fails once the board is powered and running firmware. |
| Functional test + burn-in where required | Whether the assembly does its job: powers up, runs firmware, meets its measurements, survives thermal cycling. | Why it failed. Functional test tells you a board is bad; finding the cause is a separate, manual step. |
Cost rises as you go down this table, and the rise is not linear: SPI and AOI scale roughly with volume, while ICT and functional test bring their own one-time cost in fixturing, programming and test development. That is why the answer to "how much testing" depends on quantity as much as on the product — see where the cost goes in small-batch PCBA.
How to decide how far up the ladder to go
Three questions settle it for most products.
1. What does a defect cost you after it ships?
This is the only question that really matters. A board in a bench instrument that gets reworked in-house is a different proposition from a board in a device that is implanted, or one that goes into a vehicle where a field failure triggers a recall. Inspection is insurance, and the premium should scale with what it covers.
2. How much of your board is hidden under packages?
A design with no BGA and no QFN gets most of its coverage from AOI. A design with one large BGA per board makes X-ray close to mandatory, because the joints under it are invisible to every optical method — and a BGA that looks perfect from above can have an open ball underneath. Fine-pitch BGAs make it more important, not less.
3. Does the product need to be proven working, or just proven built?
AOI and X-ray prove the board was made correctly. They say nothing about whether it works. If your product is safety-related, goes through regulatory approval, or is expensive to service in the field, you need functional test — and probably a record of it, per unit. If it is a development board or a low-risk accessory, a well-run AOI plus a power-on check may be enough.
First article inspection, and when it is required
FAI — first article inspection — is the full dimensional and visual verification of the first unit built, against the drawing and the standard, before the rest of the batch is released. It is not a sample check at the end; it is a gate at the start, and it is the point at which a process that is going to be wrong is stopped while only one board is scrap.
In automotive work FAI is part of the PPAP submission and is not optional. In medical work it is part of process validation. For most other products it is a judgement call — but it is the cheapest possible way to catch a stencil error, a wrong footprint or a mis-loaded feeder, and we would rather run it than discover the same fault in 500 boards.
Relevant standards: bare boards are inspected to IPC-A-600, assembled boards to IPC-A-610. These are different documents covering different stages, and they are commonly confused — see what IPC-A-610 Class III actually requires.
What testing does not guarantee
Two things follow from that, and they are worth asking any supplier directly. First: which inspections run on every board, and which are sampled — the answer is usually different from what the marketing implies. Second: what inspection records are kept and for how long, because in automotive and medical work the record is part of the deliverable, not a by-product.
Class III does not tighten the BGA void limit
The assumption is that every criterion gets stricter as you climb the classes. For voiding, it does not — and the difference matters when you are writing the requirement.
IPC-A-610 applies one limit across the classes: a void covering more than 25% of the X-ray image area is a defect, and there is no separate, lower figure for Class III. Older revisions of the standard said 30%, which is a good reason two suppliers can quote different numbers and each be reading their own copy of the document.
What Class III changes is not the percentage but the coverage: every board goes under the tube rather than a sample of them. That is where the extra cost and the extra assurance actually come from.
So where do the tighter numbers come from?
Suppliers who quote a smaller Class III figure — commonly around 9% of ball area, or 4% at the package interface — are usually drawing on IPC-7095, the BGA design and assembly guide. That document is a process guide, not an acceptance standard: it describes how voids form, how to measure them and how to control the process. Putting its numbers in a contract is perfectly reasonable, but it is a target the customer is adding on top, not something IPC-A-610 already imposes. Ask which document the number in the report came from.
- Ask for coverage, not just criteria. What percentage of boards went through X-ray, and was that 100% or a sampling plan?
- Ask for one number per joint. A single percentage for the whole component cannot show that one ball failed while the other four hundred passed.
- Ask what it does not measure. 2D X-ray reports how large a void is. It does not tell you where in the joint it sits, and position is what decides whether a void matters over the life of the product.
Common questions
Does AOI catch every defect?
No. AOI is an optical check: it compares what the camera sees against a programmed reference. It cannot see under a BGA, a QFN or any package whose joints are hidden beneath the body. It also produces false calls on joints that are electrically fine but look unusual, and it grades a joint as good or bad — it cannot tell a sound joint from one that will fail in six months. AOI replaces visual inspection; it does not replace electrical test.
What does X-ray add that AOI cannot?
X-ray sees through the package, so it inspects the joints AOI is blind to: BGA balls, QFN thermal pads and through-hole barrels. 3D X-ray (CT) additionally shows the shape of each joint rather than a flat overlapping shadow, which is what lets it distinguish an open joint from a good one under a dense array. It is slower and more expensive per board than AOI, so it is usually applied to the parts that need it rather than to the whole assembly.
Do I need an ICT fixture?
Only above a few thousand units of a stable design. ICT uses a bespoke bed-of-nails fixture, which is a one-time cost that has to be spread across the volume. Below that, flying-probe test or functional test usually costs less for the same coverage. The other precondition is test points: if your layout does not bring the nets out to accessible pads, a fixture cannot reach them.
Is there a stricter BGA void limit for IPC-A-610 Class III?
No, and this is the assumption most often wrong. IPC-A-610 applies one void limit across the classes: a void covering more than 25% of the X-ray image area is a defect, with no separate lower figure for Class III. Older revisions said 30%. What Class III changes is coverage - every board is X-rayed rather than a sample. Tighter figures such as roughly 9% of ball area come from IPC-7095, which is a BGA design and process guide rather than an acceptance standard, so if your contract cites them, they are a target the customer added.
Related guides
What IPC-A-610 Class III actually requires
The difference between Class I, II and III, and which products genuinely need the strictest one.
Which quality certification do you need?
ISO 9001, IATF 16949 and ISO 13485 compared — and a ten-minute check to run on any certificate.
Why 100 boards cost so much per unit
Test fixtures are one of the one-time costs that dominate a small-batch quote. Here is the full list.